
Roll forming systems for
Supermarkets uprights

 Attenzione slide vuota

- Attenzione slide vuota
Technical sheet:
| Thickness | up to 3 mm |
| Production speed | around 18–20 m/min |
| Setup time | Less than 10 min |
| Flexible roll forming technology | Interchangeable, Twin |
Roll Forming Lines for Supermarket & Shop Shelving Uprights
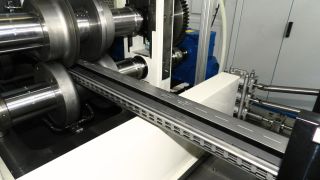
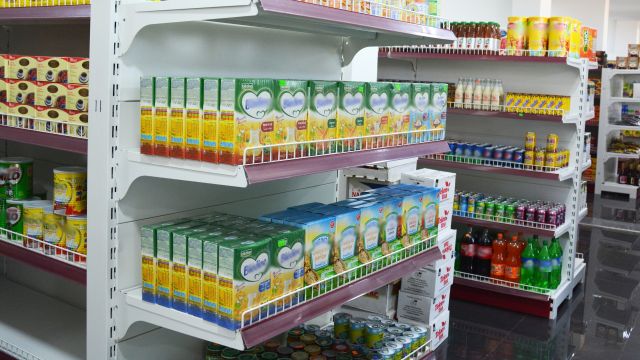
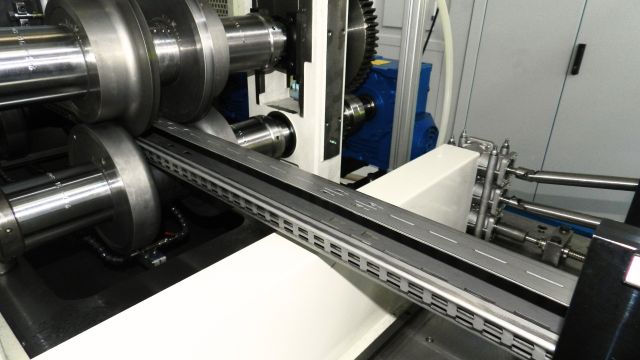
Gasparini S.p.A.’s roll forming lines for supermarket shelving uprights produce shop shelving uprights with precision punching, optimizing the production of punched profiles for the retail sector. Our roll forming systems for supermarket shelving uprights are designed to integrate decoiling, strip feeding, punching, roll forming, cutting, and additional operations such as notching and end forming.
The production challenges of retail shelving uprights
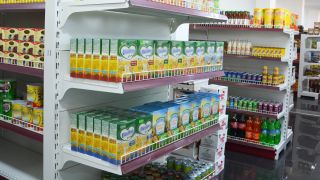
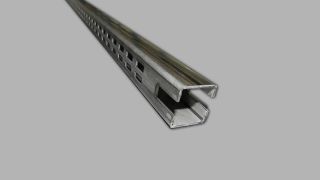
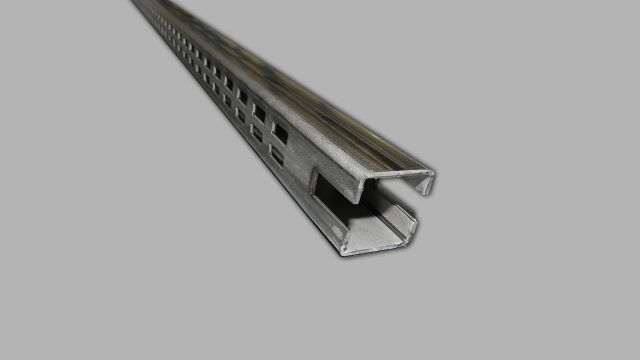
Our roll forming lines for uprights produce the profile that forms the vertical load-bearing column of supermarket shelving. It is a closed rectangular-section profile, manufactured by roll forming followed by longitudinal welding, and characterized by a high number of holes distributed along its entire length. These holes accommodate the hooks and cross members supporting the shelves, and their positional accuracy is essential to ensure interchangeability and correct in-line assembly.
Technical specifications for roll forming lines for supermarket shelving uprights
| Feature | Specifications |
|---|---|
| Product | Uprights for supermarket shelving |
| Profile section | Closed rectangular section, longitudinally welded |
| Material | Pickled steel |
| Lengths | From 1,500 to 2,500 mm |
| Roll forming system | PRO with spacers (production changeover ~1 hour) |
| Punching | High-frequency in-line mechanical press |
| Accumulator system | Coil joining without stopping the line, zero scrap |
| Welding | High-frequency with water cooling |
| Additional operations | Corner notching and downstream head/tail operations |
| Industry 4.0 integration | Bidirectional interface with customer's MES |
Punching in upright production
The main technical challenge of the line is the punching stage. The upright requires a high number of holes per unit length, which calls for the use of an in-line mechanical press – more robust and faster than hydraulic solutions – and this directly affects the maximum speed achievable by the line. The actual productivity of the system largely depends on the density and complexity of the punching pattern required.
Additional processing operations for shop shelving uprights
Some operations on the upright cannot be integrated into the in-line punching stage. Notching operations or end-forming processes – required to prepare the ends of the profile – are carried out after cutting, as supplementary stations downstream of the main line. The system configuration must include this stage in order to deliver a fully finished upright without external reworking.
How Gasparini’s roll forming line for uprights is structured
Gasparini designs the line as an integrated, sequential production system in which each station is sized to support the productivity of the others. Below is the process sequence:
- Decoiler and strip feeding – the coil of pickled steel strip is loaded onto the decoiler and continuously unwound. The material is pickled steel (not pre-painted), because the upright is painted at a later stage outside the roll forming line.
- Strip accumulator system — before punching, the accumulator allows the exhausted coil to be joined to the new one without stopping the line. The accumulator stores the strip during the joining stop and gradually releases it upstream of the press, ensuring continuous production and zero material scrap between one coil and the next.
- Punching with mechanical press — the in-line mechanical press performs the complete punching pattern on the flat strip before the material enters the roll forming stations. The use of a mechanical press is driven by the need to sustain high-frequency cycles due to the large number of holes per linear meter.
- PRO roll forming system with spacers — the roll forming stations progressively bend the strip into the final upright cross-section. The PRO system with spacers allows the production of uprights with different base widths and heights through a changeover setup of approximately one hour, making it ideal for production runs with batches long enough to absorb setup time.
- High-frequency welding with water cooling — the upright’s closed rectangular section is obtained by closing and longitudinally welding the open profile. High-frequency welding technology ensures continuity and weld quality, while water cooling manages the heat generated by the process.
- Additional end-forming operations — after cutting, dedicated stations perform notching and end operations on the upright that cannot be carried out during punching or roll forming.
- Cutting unit — the profile is cut to the programmed length, from 1,500 to 2,500 mm.
PRO system with spacers
For companies producing display uprights and supermarket shelving uprights in multiple profile types, the PRO system offers:
- Size changeover to produce different base widths and heights (setup time approx. 1 hour)
- Interchangeable cassettes for modifying profile geometry
- Greater flexibility and productivity, with less scrap, by integrating a strip accumulator before punching. This device allows us to weld the new coil to the strip already running in the line without stopping production during coil joining.
The accumulator system: how Gasparini solves line stoppages
In roll forming lines with high-frequency welding, coil changeover is a critical moment for productivity. Without an accumulator system, the line must be stopped to join the exhausted coil to the new one. Stopping and then re-accelerating the line generates 3–4 meters of strip scrap at every coil change, in addition to machine downtime.
Gasparini’s accumulator system eliminates both issues:
- The line continues producing during coil joining, with no interruptions
- The accumulated strip is gradually released upstream of the press during the joining stop
- Zero material scrap between one coil and the next
- The productivity of the roll forming system is no longer affected by the frequency of coil changes
This solution is particularly relevant for high-volume production, where every minute of downtime directly translates into production cost.
Punching accuracy for shelf engagement
Punching is a key element of the line because it determines both the modularity and the reliability of shelf engagement. The punching system often relies on a mechanical press to manage the high number of holes required on the upright.
This level of accuracy is essential for upright production lines intended for display and retail shelving systems.
Welding system
High-frequency welding with water cooling is normally recommended for this type of production. When this welding technology is used, some customers request a strip accumulator system before punching, allowing a head-to-tail joint between the old coil and the new one without stopping the machine. The main benefits are the elimination of scrap and the avoidance of machine downtime.
Line speed and productivity
Gasparini roll forming lines for supermarket shelving uprights are designed for high productivity:
- Typical operating speed: around 18–20 m/min
- Lengths: from 1 to 2.5 m
- Material: pickled steel
- Typical thicknesses: up to 3 mm
- Possibility of integration with end-of-line operations and strapping and labeling systems to optimize workflow
Industry 4.0 integration
The roll forming line for supermarket shelving uprights connects to the customer’s MES system through a bidirectional interface: production programs are automatically uploaded to the machine, while process data are recorded batch by batch. This ensures full traceability of processed material and production aligned in real time with plant scheduling.
Configure the roll forming line for your uprights
The production needs of each retail shelving manufacturer are different: sections to be produced, volumes, product mix, and process integration all determine the optimal system configuration. Gasparini’s engineering team analyzes your specific case and defines the most efficient solution.
We can support you in evaluating:
- Mechanical press configuration according to the punching pattern required for your upright
- Accumulator system sized to your production volumes and coil change frequency
- Selection of the most suitable roll forming system based on your dimensional or profile geometry mix
- Integration of supplementary end-forming operations into the line sequence
- Optimization of production logic to reduce downtime and maximize hourly productivity
Fill out the contact form to receive tailored technical advice for your upright line or for roll forming lines for supermarket shelving